|
Acrylic Sheet
Wallis
| Color: | |
|---|---|
| Size: | |
| Material: | |
| Quantity: | |
Virgin White Sanitary Acrylic Sheet for Bathtubs and Showers
Wallis virgin white sanitary acrylic sheet is a high-gloss PMMA material developed for thermoformed bathtubs, shower trays, washbasins, tub liners and sanitary panels. It is supplied to bathroom-fixture manufacturers, vacuum-forming factories, sanitary ware brands, project contractors, importers and material distributors requiring consistent color, clean surfaces and repeatable forming performance.
The sheet can be produced in white and customized sanitary colors, with thicknesses and dimensions selected around the mold depth, draw ratio, final wall thickness and reinforcement process. Virgin PMMA provides a smooth, non-porous decorative surface that can be polished and repaired when minor surface damage occurs.
Bathtubs and shower products are complete engineered assemblies. Depending on the design, a formed virgin-PMMA shell may be combined with fiberglass reinforcement, support framing, suitable adhesives or structural backing. PMMA/ABS is a separate composite material category, not another name for monolithic virgin PMMA. Validate the full fixture construction rather than evaluating raw sheet properties alone.
| Material | Virgin PMMA sanitary acrylic sheet; composite structures subject to project requirements |
| Primary Applications | Bathtubs, shower trays, tub liners, washbasins, sanitary panels and bathroom fixtures |
| Thickness Range | 3–10 mm reference range; availability depends on grade, dimensions and order quantity |
| Surface | High-gloss, smooth, non-porous sanitary surface with protective masking |
| Processing | Vacuum forming, pressure forming, trimming, drilling, bonding and reinforcement after validation |
| B2B Services | Samples, custom color matching, OEM dimensions, forming trials, inspection and export packaging |
Request Sanitary Acrylic Samples and Quote
The table summarizes indicative values for the sanitary PMMA range. Mechanical and thermal properties depend on the exact resin formulation, manufacturing process and test conditions. Confirm tolerances, test reports and the approved technical data sheet for the supplied grade before purchasing.
| Property | Test Reference | Unit | Listed Value | Procurement Note |
|---|---|---|---|---|
| Specific Gravity | Confirm with grade TDS | — | 1.19 | Typical PMMA density |
| Tensile Strength | GB/T 1040.1 | MPa | ≥70 | Flat-sheet result; formed-part performance varies |
| Flexural Strength | GB/T 9341 | MPa | ≥98 | Reinforcement and product geometry affect stiffness |
| Vicat Softening Temperature | GB/T 1633 | °C | ≥110 | Test condition and load must be specified |
| Recommended Long-Term Temperature | Project-specific | °C | Up to 70 listed | Depends on load, duration and complete fixture design |
| Thickness | Order specification | mm | 3–10 | Select by draw ratio and minimum formed wall |
| Standard Panel Sizes | Order specification | mm | 1230 × 2450 / 1250 × 1850 / 1400 × 2200 | Custom sizes subject to production and yield |
| Color | Approved physical sample | — | White and custom sanitary colors | Specify gloss, opacity, whiteness and ΔE tolerance |
| Surface Performance | Customer-agreed methods | — | High-gloss sanitary surface | Define scratch, stain and cleaner-resistance tests |
For an opaque white sanitary acrylic sheet, buyer acceptance should focus on whiteness, opacity, CIELAB color coordinates, surface gloss and color difference between approved and production samples. A light-transmission figure for clear PMMA does not describe the appearance of an opaque white grade.
Controlled virgin resin, pigments and processing help deliver uniform color and a smooth high-gloss surface. For repeat production, whiteness, gloss and allowable color difference should be measured against an approved physical reference rather than described only as “pure white.”
Sanitary acrylic grades are selected for heating, stretching and reproducing the curved geometry of tubs and shower trays. Deep draws require controlled sheet temperature, mold design, clamping, plug assistance and adequate starting gauge to reduce thinning, tearing and punctures.
The smooth PMMA surface does not contain grout lines and is easy to wipe with compatible household bathroom cleaners. Hygiene performance also depends on product geometry, joints, water drainage and cleaning practices; the raw sheet should not be marketed as self-sterilizing.
Minor surface marks may be sanded and polished by trained personnel when the material thickness and finish allow it. Deep cracks, stress damage and structural defects require professional evaluation rather than cosmetic polishing.
White, cream, black, solid colors and project-specific shades can be discussed. Color should be evaluated after thermoforming because stretching, thickness reduction and lighting can change the perceived shade.
Clean PMMA production offcuts may be recyclable through suitable specialist channels. Actual recovery depends on contamination, protective film, reinforcement materials, local infrastructure and applicable waste regulations.
Gloss and Color Consistency
Sanitary-Grade Thermoforming
For bath and shower production, “white” is not a single universal color. A bright blue-toned white, neutral white and warm ivory can look different under factory lamps, showroom lighting and natural daylight. Agree a physical master sample, viewing conditions and acceptance limits before production.
| Acceptance Parameter | What the Buyer Should Define | Why It Matters |
|---|---|---|
| White shade / CIELAB | Approved master panel, L*, a*, b* values and measurement illuminant | Prevents visible differences between bathtub shells, shower trays and matching accessories |
| Color difference (ΔE) | Measurement geometry and permitted ΔE limit by project | Supports consistent repeat orders; do not assume one tolerance for all applications |
| Opacity / hiding power | Minimum opacity at the finished thin-wall area | Reduces show-through of framing or backing after deep drawing |
| Surface gloss | Measurement angle and accepted reference value | Helps align appearance across formed parts and surface finishes |
| Defect acceptance | Inspection lighting, distance and criteria for bubbles, black spots and scratches | Creates objective incoming and final-part acceptance rules |
| After-forming appearance | Color and gloss at representative deep-draw zones | Confirms visual quality under the actual production cycle |
Test the chosen white grade on the actual mold, including corners and areas of maximum stretch. Color and optical appearance should be checked after forming and reinforcement, not only on an unformed flat sample.
| Structure | Typical Advantage | Selection Consideration |
|---|---|---|
| Monolithic Virgin PMMA | Uniform acrylic composition, high-gloss face and repairability through the sheet thickness | Often requires separate reinforcement in large fixtures |
| PMMA/ABS Co-Extruded Sheet | Acrylic decorative face combined with a tougher or more economical backing layer | Cap-layer thickness, adhesion and forming behavior must be specified |
| Acrylic Shell + FRP Reinforcement | Adds stiffness and support to a formed tub or tray shell | Resin, glass content, curing, odor and interface adhesion require process control |
| Engineered Composite Backing | Can improve rigidity, production efficiency or reduce fiberglass use | Complete composite should be qualified as one product system |
Sanitary PMMA sheets can be formed into freestanding, alcove, corner, whirlpool and massage bathtub shells. The sheet thickness should be chosen from the mold size, depth, radii, expected wall thinning and reinforcement system—not from one universal bathtub gauge.
White acrylic is suitable for molded shower trays with integrated slopes and drain areas. Slip resistance is a finished-product requirement and may require a molded texture, coating or separate test; a smooth gloss sheet should not automatically be described as anti-slip.
PMMA can be used for washbasin shells, vanity components, sanitary covers and decorative bathroom parts where high gloss, color matching and easy cleaning are required.
Thermoformed liners can be designed for renovation systems. Accurate measurement, compatible adhesives, trapped-moisture control, perimeter sealing and substrate condition are essential to long-term performance.
Flat or formed PMMA panels can provide a seamless decorative surface. The complete wall system must include suitable backing, movement allowance, joint design and sealant. A panel alone does not guarantee a waterproof installation.
Sanitary Ware Applications
Shower and Bathroom Panels
Bathtub and Tub Liner Production
Thermoformed Acrylic Bathtub
High-Gloss Sanitary Finish
| Factor | Sanitary Acrylic | Gel-Coated FRP | Enamel / Ceramic | Solid Surface |
|---|---|---|---|---|
| Surface Appearance | High-gloss, smooth and color-matched | Depends on gel-coat quality | Hard glazed surface | Matte to satin; some gloss options |
| Forming and Design | Suitable for vacuum and pressure forming | Molded composite process | Limited by ceramic or metal process | Fabricated or cast; grade-dependent forming |
| Weight | Relatively lightweight | Relatively lightweight | Often heavier | Often heavier |
| Repairability | Minor marks may be polished | Gel-coat repair possible | Chips can be difficult to match | Often sandable and repairable |
| System Requirement | Usually requires reinforcement and support | Composite lay-up is structural system | Requires suitable base and installation | Requires engineered support and joints |
A bathtub manufacturer should select sheet grade and starting thickness from the completed part geometry, required minimum wall thickness and reinforcement design. A thicker starting sheet does not by itself guarantee uniform walls after deep drawing.
| Project Variable | Procurement Check | Typical Production Risk |
|---|---|---|
| Mold depth and draw ratio | Provide sectional drawings and desired forming direction | Excessive wall thinning at deep corners or steep walls |
| Radii and drain geometry | Identify tight corners, holes and detailed features | Stress concentration, cracking and incomplete forming |
| Starting gauge / tolerance | Confirm full-width thickness profile, not only nominal gauge | Inconsistent heating and finished-part stiffness |
| Cast vs. extruded PMMA | Identify exact grade, sheet process and manufacturer-approved forming procedure | Wrong heating or drying assumptions for the selected material |
| Reinforcement design | Specify FRP resin, adhesive, foam, base and support requirements | Delamination, residual stress or inadequate structural rigidity |
| Water and chemical exposure | Define hot-water cycle, cleaning products and stain tests | Crazing, discoloration or premature surface damage |
For a first-time mold, use a controlled pilot run to verify sag, formed wall distribution, color, crack resistance and attachment to the selected backing. Record the approved material code, gauge and process settings for repeat purchases.
Define the finished fixture: Supply the mold drawing, overall size, cavity depth, radii, draw ratio and minimum wall-thickness target.
Select the sheet structure: Choose monolithic PMMA, PMMA/ABS or another approved sanitary composite.
Approve color and surface: Confirm white shade, gloss, opacity, protective film and visible-face orientation.
Condition and dry if required: Follow the exact grade's storage and pre-drying guidance to reduce bubbles and surface defects.
Develop the heating profile: Heat uniformly and measure actual sheet temperature rather than relying only on heater settings.
Form and cool: Optimize vacuum, pressure, plug assistance, mold temperature and controlled cooling.
Trim and reinforce: Validate cutting, drilling, backing, frame bonding and support-base installation.
Test the finished product: Inspect wall distribution, color, gloss, cracks, drainage, load, hot-water cycling, cleaners, leaks and applicable sanitary standards.
A trial sheet-temperature range of approximately 160–185°C may be relevant to certain PMMA formulations, but it is not a universal processing recommendation. The appropriate window depends on sheet grade, cast or extruded process, thickness, pigment, heating equipment, mold geometry and cycle time. Do not equate heater setpoint with actual sheet temperature.
Underheating can cause incomplete forming, high residual stress and poor detail reproduction. Overheating can cause excessive sag, bubbles, surface damage, sticking or degradation. Production parameters should be established from the approved grade's data and forming trials.
The same sheet can behave differently on different molds and machines. The following troubleshooting points are starting hypotheses; determine the root cause through production trials and supplier technical data.
| Observed Problem | Possible Causes | Recommended Check |
|---|---|---|
| Bubbles or blisters | Absorbed moisture, surface contamination or overheating | Check conditioning/drying instructions and actual sheet temperature |
| Whitening at corners | Excessive strain, low forming temperature or tight mold radii | Review draw depth, corner design, heater balance and starting thickness |
| Thin spots or tearing | Uneven heat, excessive draw ratio or inadequate plug assistance | Map wall thickness after forming and revise mold/process settings |
| Cracks after trimming | Machining stress, sharp edges or inadequate support | Inspect tool geometry, support and residual stress |
| Surface haze or gloss loss | Overheating, contamination or wrong contact surface | Inspect heater profile, mold finish and protective masking |
| Uneven white color | Pigment distribution, material thickness variation or excessive stretching | Compare approved master and post-form CIELAB readings |
| Backing delamination | Poor surface preparation or incompatible reinforcing resin | Evaluate interface preparation, cure cycle and peel performance |
Before a commercial production order, establish an acceptance plan covering minimum formed wall thickness, visual appearance, dimensional stability, backing adhesion and any finished-product safety requirements.
Use sharp, suitable saw or router tools with stable support. Control heat and vibration to reduce chipping, melting and stress. Keep protective film in place where practical during fabrication.
Adhesives, reinforcing resins, foam and backing materials must be compatible with PMMA and the production process. Solvent attack, exothermic heat, shrinkage and poor interface adhesion can cause crazing or delamination.
Finished tubs and trays require engineered rims, frames, feet or bases to distribute user and water loads. The decorative acrylic shell should not be treated as the only structural component unless the complete design has been qualified accordingly.
Use sealants approved for PMMA and the adjoining construction materials. Waterproof performance comes from the complete assembly, including substrate preparation, joints, drain connections, movement allowance and maintenance.
Thickness profile: Average gauge and cross-sheet thickness distribution.
Sheet dimensions: Length, width, squareness and edge quality.
Surface appearance: Scratches, black spots, gels, bubbles, flow lines and protective-film condition.
Color and gloss: Whiteness, opacity, gloss and color difference versus the approved sample.
Thermoforming test: Sag behavior, mold reproduction, thinning, tearing, bubbles and post-form color.
Mechanical properties: Tensile, flexural, impact or other project-specific tests.
Chemical and stain testing: Approved bathroom cleaners, dyes, oils and personal-care products.
Finished-fixture validation: Load, thermal cycling, drainage, leak, slip and applicable sanitary-product requirements.
“Virgin PMMA” describes a material-source requirement, not a result that can be proven from sheet appearance alone. Buyers who require virgin resin should request a written raw-material declaration and define whether regrind, recycled content or processing scrap is permitted under their specification.
| Document or Check | Purpose |
|---|---|
| Approved TDS | Confirms material grade, thickness, relevant properties and declared test conditions |
| Raw-material declaration | Documents virgin-resin or recycled-content requirements for the agreed product |
| Color master and sample approval | Provides a repeatable white-color and gloss reference |
| Certificate of analysis or inspection report, if agreed | Supports incoming verification for the agreed batch and tested properties |
| Lot and packing identification | Enables traceability of samples, shipments and repeat orders |
| Forming trial and finished-product qualification | Confirms performance of the actual shell, backing and installation system |
For projects subject to specific sanitary-ware standards, confirm the destination market and applicable finished-product tests. A general-purpose PMMA data sheet should not be presented as certification of a completed bathtub or shower tray.
| Sheet Structure | Monolithic PMMA or project-specific composite structure subject to availability |
| Thickness | 3–10 mm reference range, with project-specific tolerances subject to confirmation |
| Dimensions | Standard formats or custom sheet size based on mold and production yield |
| Color and Gloss | Sanitary white, cream, black and custom colors with physical sample approval |
| Protective Masking | Thermoforming-compatible film or paper masking subject to process |
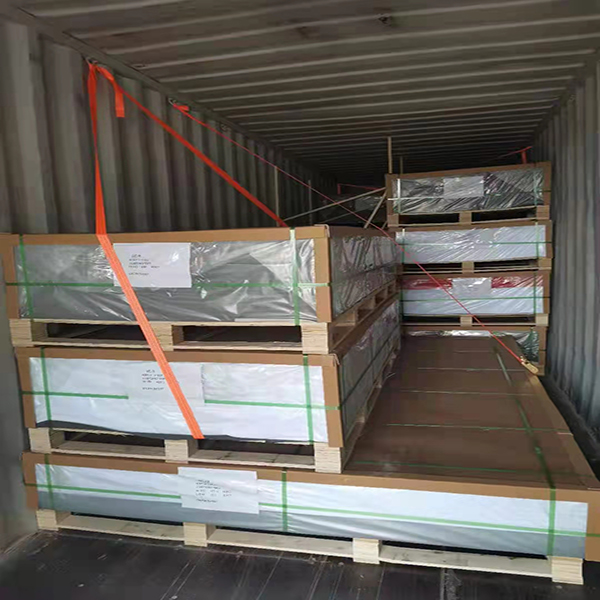
| Packaging | PE protection, kraft paper, reinforced pallets, corner protection and custom labels |
High-gloss sanitary acrylic sheets require clean handling and surface protection throughout storage, conversion and shipment. Sheets should be supported flat, protected from scratches and secured against movement during international transportation.
Protected Export Pallet
Container Loading for Bulk Orders
Application-based selection: Sheet structure, thickness and dimensions are reviewed against the mold and finished fixture.
Sample-first process: Buyers can evaluate color, gloss, forming and reinforcement before volume orders.
OEM customization: Sanitary colors, dimensions, masking and packaging can be discussed.
Batch specification control: Key requirements can be recorded against approved samples and data sheets.
Export-ready packaging: Protective pallet solutions support international supply.
B2B project support: Suitable for bathtub factories, thermoformers, sanitary brands, importers and distributors.
Global B2B Project Coordination
For repeat sanitary projects, Wallis can coordinate approved color references, technical specifications, packaging and delivery schedules. Buyers should retain signed samples from both flat sheet and thermoformed parts because color and gloss may change after processing.

Finished product: bathtub, shower tray, basin, liner or wall panel.
Monolithic PMMA, PMMA/ABS or other required sheet structure.
Required thickness, dimensions, quantity and annual forecast.
White shade, gloss, opacity, color reference and tolerance.
Mold dimensions, cavity depth, draw ratio and minimum formed wall.
Forming machine, heater type, clamping and plug-assist process.
Reinforcement, backing, adhesive, frame and support-base system.
Required sanitary standards, chemical tests and destination market.
Protective film, pallet, labels and delivery schedule.
Sample dimensions, destination port and trade terms.
Discuss Your Bathtub or Shower Project
It is a PMMA sheet formulated and produced for thermoformed bathroom fixtures such as bathtubs, shower trays and basins. Important properties include forming response, color, gloss, chemical resistance and surface quality.
They serve different design and cost targets. Monolithic virgin PMMA offers acrylic properties throughout the thickness, while PMMA/ABS combines an acrylic face with a backing layer. The correct choice depends on forming, reinforcement, repairability and budget.
Many projects begin with approximately 3–6mm sheet, but no single gauge fits every tub. Mold depth, draw ratio, wall-thickness target, reinforcement and finished load requirements determine the correct starting thickness.
Some PMMA grades may be trialed around 160–185°C, but the correct forming window depends on the approved material grade and measured sheet temperature. Establish validated conditions through controlled trials with the production mold.
Most large tubs and trays require reinforcement, frames, bases or engineered composite backing. The required system depends on shell geometry, wall thickness, load and applicable product standards.
PMMA does not absorb water like porous building materials, but a bathtub, shower wall or tray is waterproof only when joints, drain connections, seals, backing and installation are correctly designed.
Color stability depends on resin, pigment, stabilizers, heat history, cleaner exposure and UV conditions. Specify the expected environment and approve a grade with suitable aging or color-stability data.
Use mild, non-abrasive cleaners approved for acrylic. Avoid abrasive pads and unverified solvents. The finished fixture manufacturer should publish a validated care guide for end users.
Minor surface scratches may be sanded and polished by trained personnel. Deep damage, cracks or areas with insufficient remaining thickness require a professional repair assessment.
Custom color matching can be discussed. Buyers should provide a physical master sample and define lighting, gloss, opacity and acceptable color difference before production.
Yes, suitable sheets can be used as decorative wall surfaces. The complete wall assembly requires compatible backing, adhesives, movement allowance and sealed joints.
Yes. Flat-sheet and thermoforming trials are recommended for evaluating color, gloss, thickness, sag, wall distribution, reinforcement adhesion and finished-part appearance.
MOQ depends on sheet process, structure, thickness, size, color, masking, packaging and whether the specification is standard or customized.
Provide the finished fixture, sheet structure, gauge, dimensions, color, quantity, mold, forming process, reinforcement, standards, packaging and destination.
Ask for a grade-specific material declaration, applicable technical documents and batch traceability. Appearance alone cannot confirm whether recycled or reprocessed content was used.
Deep drawing reduces local wall thickness, which can change opacity, gloss and perceived color. Confirm the final shade using formed samples at the thinnest areas under agreed lighting conditions.
Possible factors include unsuitable conditioning, excessive or uneven heating, surface contamination and excessive local stretch. Review the exact material grade, sheet temperature, mold geometry and process records.
No. PMMA/ABS is a multilayer construction containing an ABS backing. If the purchase requirement is monolithic virgin PMMA, specify that exact construction and confirm it in the technical documents.
Agree in advance on grade identification, thickness tolerance, approved white-color sample, batch or lot number, inspection results, packing list and any required material declaration or technical report.
Contact Wallis Plastic for virgin white PMMA sheets for bathtub shells, shower trays, tub liners, basins and sanitary panels. Our team supports material selection, custom colors, forming trials, OEM specifications, protective packaging and factory-direct B2B supply.
Request Samples and Factory Quote