Wool Silicone Press Pad for PVC, PETG & PC Card Lamination
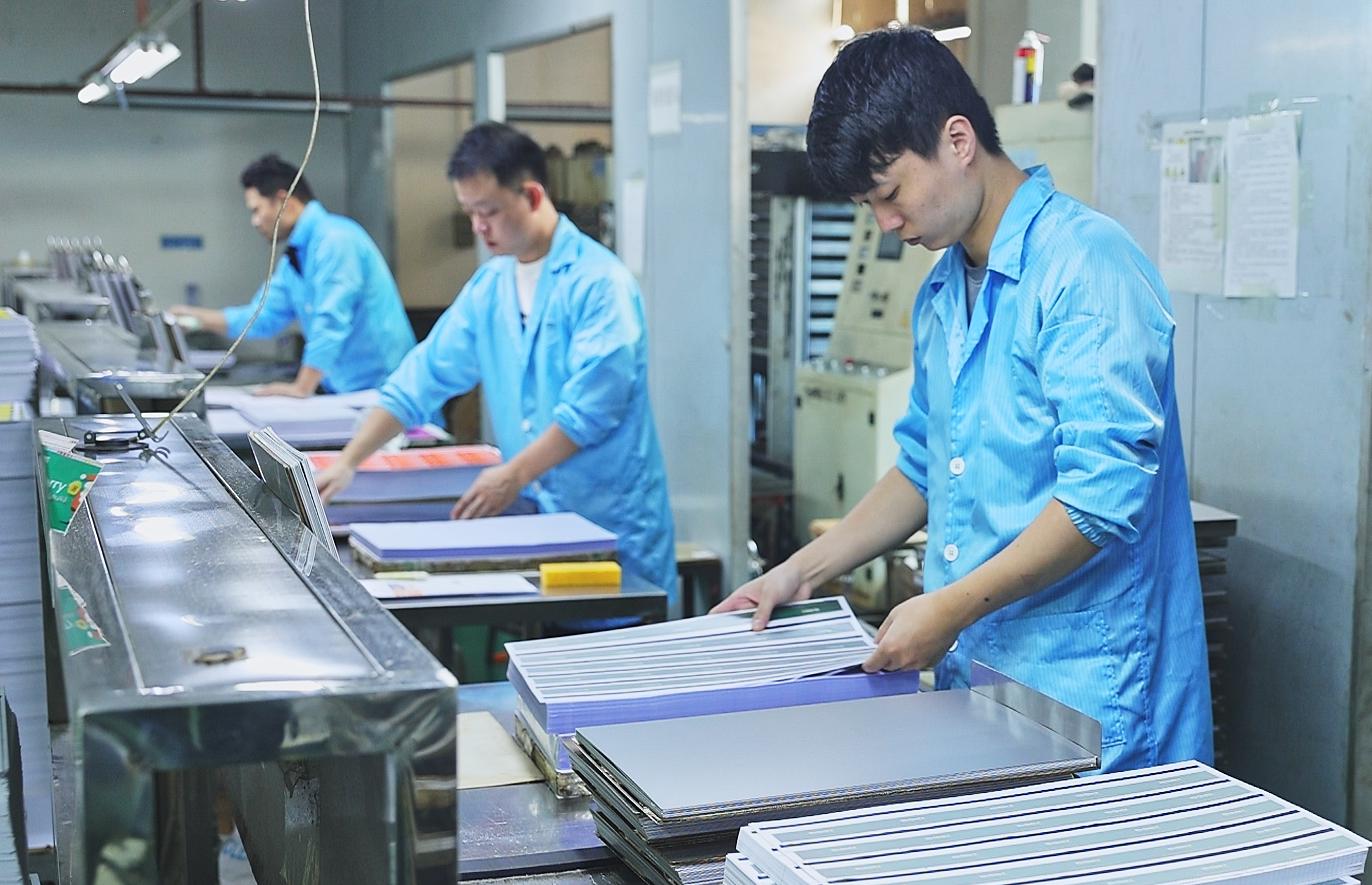
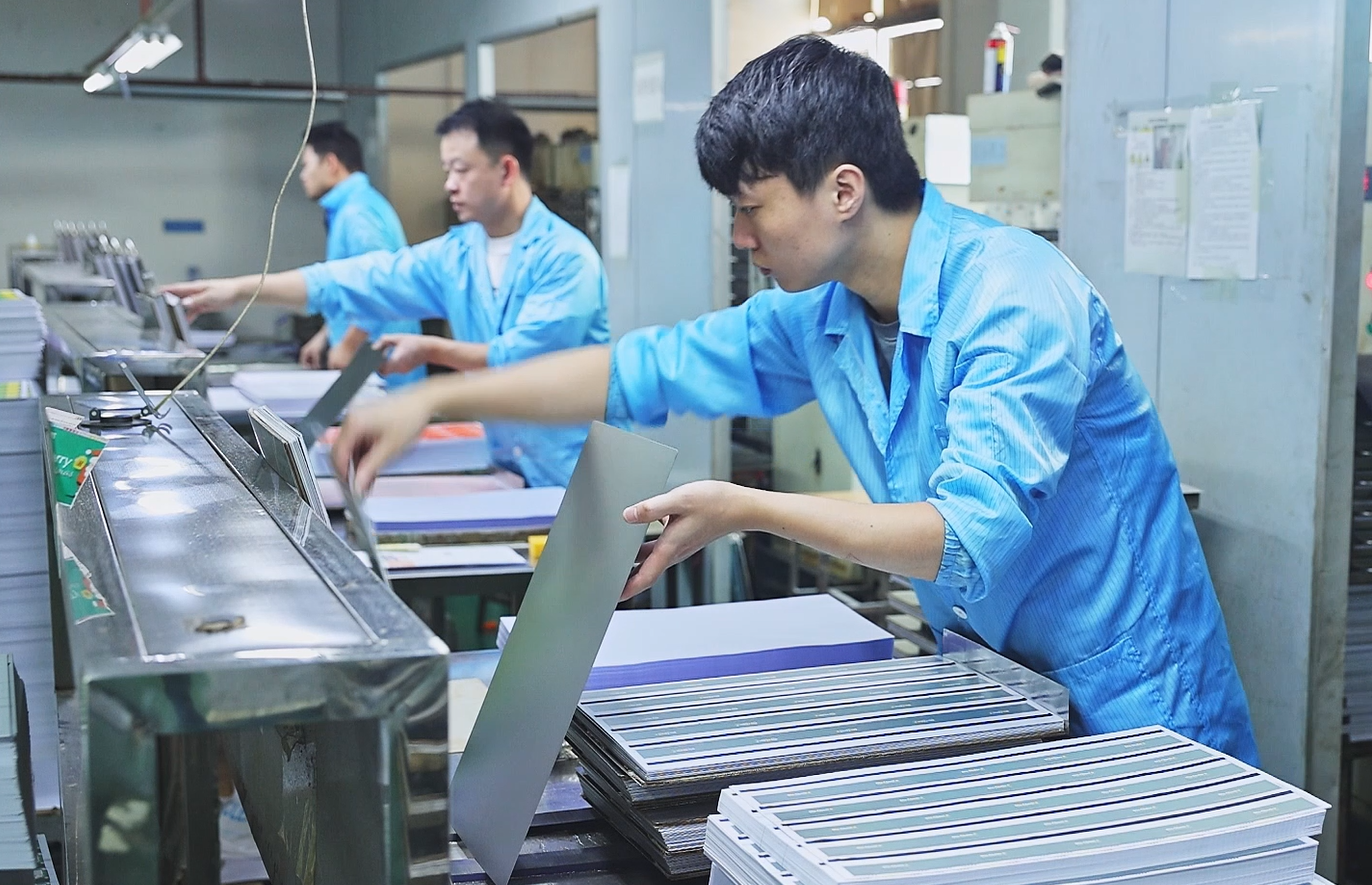
Wallis wool silicone press pad for card lamination is a heat-resistant cushioning material designed for industrial hot-press production of PVC, PETG and polycarbonate cards. The current construction combines heat-resistant silicone with a wool felt cushioning layer to support controlled pressure distribution during repeated card lamination cycles.
Available in 3mm, 5mm, 8mm and 10mm thicknesses, with customized dimensions, density and shapes, the pad can be matched to different lamination plates, card-sheet formats and press configurations. The current Wallis specification describes heat resistance up to approximately 180°C for typical PVC, PETG and PC card-lamination conditions.
Typical applications include bank cards, ID cards, membership cards, smart cards, contactless cards, multi-layer plastic cards and overlay-film lamination. The wool-felt cushioning structure differentiates this product from Wallis silicone-only and silicone-fiberglass press-pad products.
For professional B2B selection, buyers should provide the laminator model, heating-plate dimensions, current pad thickness, card material, hot-press temperature, pressure, dwell time, cooling conditions and expected production cycles. These parameters should be evaluated together rather than selecting a pad only by thickness.
Wool Silicone Press Pad Specifications
| Specification / Attribute | Standard / Custom Option |
| Pad Material | Heat-resistant silicone + wool felt base |
| Heat Resistance | Suitable for typical PVC, PETG and PC card lamination temperatures — currently stated up to approximately 180°C |
| Thickness Options | 3mm / 5mm / 8mm / 10mm; custom thickness available per order |
| Pad Size / Dimensions | Customized to match lamination plate dimensions; OEM/ODM supported |
| Pressure Distribution | Designed to support more uniform pressure distribution across the usable pad surface |
| Surface Contact | Smooth silicone surface described as non-abrasive to card overlays |
| Durability / Lifespan | Reusable for repeated lamination cycles under suitable process and maintenance conditions; exact cycle life is not currently published |
| Edge / Shape | Rectangular or custom-cut shape to match the lamination plate |
| Order Quantity / MOQ | Current page describes flexible small-batch and bulk ordering; confirm exact MOQ for the selected specification |
| Customization & OEM/ODM | Custom size, thickness, density and shape according to laminator requirements |
Technical clarification: the current Wallis product specification describes this pad as heat-resistant silicone combined with a wool felt base, but it does not publish the exact wool content, felt density, silicone hardness, detailed layer orientation, thickness tolerance, compression recovery or permanent compression-set value. Buyers requiring these parameters should request model-specific technical data.
Temperature clarification: approximately 180°C is the current published value for this Wallis product. Do not replace it with a competitor's 200°C or 250°C specification unless Wallis has test data confirming the higher rating for this exact construction.
What Is a Wool Silicone Card Lamination Pad?
A wool silicone card lamination pad is a compliant hot-press cushion used inside the lamination stack of a plastic-card press. It combines the heat-resistant behavior of silicone with the cushioning characteristics of wool felt to help accommodate small differences in card-stack thickness and press conditions.
Silicone Layer
Silicone provides the heat-resistant elastomeric component of the pad. Its hardness, thickness and compression characteristics influence how the pad responds under lamination pressure.
Wool Felt Cushioning Layer
Wool felt adds a textile-based cushioning layer that can provide a softer mechanical response than some reinforced silicone constructions. Felt density, moisture condition and long-term compression should therefore be considered during production.
Combined Press Cushioning
The combination is intended to help distribute press load across the card stack while accommodating minor local thickness differences. It should be regarded as one component of the complete lamination recipe rather than a standalone solution for every card defect.
Why Wool Felt Changes Lamination Performance
Softer Cushioning Response
A felt-containing cushion may provide a softer mechanical response than a harder or more heavily reinforced silicone pad. This can be useful when the lamination stack requires additional compensation for small local variations.
Thermal Response Can Differ
Felt thickness and density can influence how quickly heat travels through the complete lamination stack. When changing from another pad construction to a wool-silicone pad, the existing heating and cooling recipe should therefore be revalidated.
Moisture Control Matters
Textile-based materials can respond differently to storage humidity than solid silicone. Keep the pad dry and clean, especially where moisture-sensitive card materials, inks or overlays are used.
Check for Lint or Surface Contamination
Any loose fibers, dust or contamination in the lamination stack can create visible marks. Inspect felt edges and exposed surfaces regularly and remove contaminated pads from production when necessary.
How Wool Silicone Pads Support Pressure Distribution
Hot-press card lamination combines temperature, mechanical pressure and controlled cooling. The cushion pad sits within this system and helps the stack respond to small dimensional differences between layers.
Compensating for Local Thickness Variation
Printed layers, RFID inlays, embedded electronic components and other card structures can introduce minor thickness variation. A compliant cushion can help reduce highly localized pressure concentrations.
Supporting Plate Contact
Correctly selected pad dimensions and thickness help maintain more consistent contact across the usable press area. Oversized, folded, contaminated or compressed pads can negatively affect this function.
Not a Guarantee Against Bubbles or Warping
Lamination defects can also result from trapped air, moisture, solvent retention, uneven platen temperature, incorrect pressure, ink-film thickness, overlay chemistry, cooling rate or poor plate parallelism. A cushion pad should therefore be selected as part of the complete process.
3mm, 5mm, 8mm & 10mm Wool Silicone Pad Options
Wallis currently lists 3mm, 5mm, 8mm and 10mm thickness options. Thickness affects the compressed stack height, pressure compensation and potentially the thermal response of the press assembly.
3mm Wool Silicone Pad
A 3mm construction can be evaluated where the press requires a relatively thin wool-silicone cushion or where the existing approved pad uses a similar thickness.
5mm Wool Silicone Pad
A 5mm pad provides additional cushioning thickness and should be validated against the laminator clearance, pressure setting and heat-transfer profile.
8mm Wool Silicone Pad
An 8mm pad may provide a deeper compliant layer, but it also changes the total lamination-stack height. Confirm machine clearance and heating conditions before replacing a thinner pad with an 8mm version.
10mm Wool Silicone Pad
A 10mm construction should be selected only after confirming that the laminator can accommodate the increased thickness and that the required temperature and pressure profile remains achievable.
Custom Thickness
Custom thickness can be reviewed for specific card presses. Providing an existing approved cushion sample or detailed drawing helps reduce replacement-pad selection errors.
Heat Resistance up to Approximately 180°C
The current Wallis specification states that the wool silicone pad is suitable for typical PVC, PETG and PC card lamination temperatures up to approximately 180°C.
Continuous Temperature vs Peak Temperature
Buyers should distinguish between a continuous operating temperature and a short-duration peak temperature. The current page does not publish separate ratings for these two conditions.
Dwell Time Matters
Exposure to a given temperature for several minutes can affect a pad differently from brief contact. Include hot-press dwell time and cycle frequency when requesting technical confirmation.
PC Lamination Requires Specific Confirmation
Polycarbonate card lamination can use demanding thermal cycles. If your actual process approaches or exceeds the current published temperature limit, confirm compatibility before ordering rather than relying on the generic PC application statement alone.
Hardness, Felt Density & Compression Recovery
Silicone Hardness
Silicone hardness affects deformation under press load. The current Wallis page states that density can be customized but does not publish a specific Shore A hardness value for this wool-silicone model.
Wool Felt Density
Felt density affects cushioning, compression and thermal behavior. If a buyer is replacing an existing felt-silicone pad, density should be compared together with thickness and hardness.
Compression Set
After repeated hot-press cycles, permanent thickness loss can reduce cushioning performance. Wallis should add a measured compression-set or thickness-loss specification if available.
Compression Recovery
Recovery after each press cycle influences long-term repeatability. High-volume card manufacturers should request applicable recovery data or perform an actual production trial.
Applications in Plastic Card Production
PVC Card Lamination
Wool silicone pads can be used in hot-press lamination of printed PVC cores and PVC overlays for ID cards, membership cards, bank cards and other plastic-card products.
PETG Card Lamination
PETG card structures can also use a compatible wool-silicone cushion. Temperature, pressure and cooling settings should be validated with the actual PETG formulation and card stack.
Polycarbonate Card Lamination
PC card production requires controlled thermal processing. Confirm the actual press temperature against the current approximately 180°C Wallis rating before production use.
RFID & Smart Card Production
Contactless-card and RFID sheets can contain antennas, inlays and local structural variation. A compliant cushion can help accommodate minor thickness differences during the lamination cycle.
Overlay Film Lamination
The current Wallis page also lists overlay-film lamination as an application. Confirm the exact stack sequence and which surface of the pad contacts the plate or release layer.
Multi-Layer Card Construction
Multi-layer card structures can benefit from controlled cushioning where repeated lamination cycles require consistent pressure distribution.
Wool-Silicone vs Silicone vs Silicone-Fiberglass Press Pads
| Pad Type | General Construction | Key Selection Points |
| Wool Silicone Press Pad | Silicone combined with wool felt cushioning | Felt density, moisture, lint, compression recovery, thickness and temperature |
| Silicone Press Pad | Silicone-based pad without the wool-felt construction described on this page | Hardness, thickness, temperature, compression behavior and surface condition |
| Silicone-Fiberglass Cushion | Silicone with fiberglass reinforcement | Reinforcement integrity, thickness, hardness, surface condition and thermal response |
There is no universally best press-pad construction for every laminator. Compare candidate pads using the same steel plates, card stack, temperature, pressure, heating time and cooling program used in your production line.
How to Select the Correct Wool Silicone Pad
1. Provide Laminator Model
Provide the laminator manufacturer, model and configuration if available. Existing pad specifications or photographs can also help identify the required construction.
2. Confirm Plate Dimensions
Supply heating-plate or cassette length and width, including any positioning holes, corner radii, cut-outs or clearance requirements.
3. Specify Existing Pad Thickness
If replacing an existing pad, measure its original specification if known rather than measuring only a heavily compressed used pad.
4. Provide Card Material
Specify PVC, PETG, PC or another material and identify overlay, inlay or special layers in the lamination stack.
5. Provide Temperature & Pressure
State normal operating temperature, maximum temperature, press pressure and hot dwell time.
6. Describe Current Lamination Problems
If replacing a pad because of defects, describe the actual problem such as pressure marks, uneven lamination, pad compression, contamination or excessive replacement frequency.
7. Run a Production Trial
Test the candidate pad with the real production stack before changing the specification across a full production line.
Cleaning, Storage & Replacement Guidelines
Keep the Pad Clean
Dust, ink residue, adhesive or card fragments can become pressure points during lamination. Inspect and clean the pad according to the approved maintenance procedure.
Keep Wool Felt Dry
Store the pad in a dry environment and avoid uncontrolled moisture exposure, particularly before high-temperature press cycles.
Store Flat
Store large sheets flat where possible to reduce unwanted bending, folding or local deformation.
Monitor Permanent Thickness Loss
Replace or re-evaluate pads that show excessive permanent compression, damaged felt, surface contamination, hardened silicone, edge damage or inconsistent lamination performance.
Do Not Use a Fixed Cycle Count Without Validation
The current Wallis page does not publish a guaranteed number of lamination cycles. Service life depends on temperature, pressure, dwell time, storage, cleaning and the pad specification.
Quality Control for Wool Silicone Press Pads
Finished length and width
Pad thickness
Thickness consistency across the sheet
Flatness
Cut-edge quality
Silicone surface condition
Wool felt condition
Layer bonding where applicable
Visible contamination
Loose fibers or damaged felt
Hardness or density where specified
Heat-resistance requirement
Compression behavior where specified
Custom holes or cut-outs
Quantity and packaging
Measure More Than One Point
Thickness should be checked at multiple positions across large pads when dimensional consistency is important to the application.
Inspect Felt Before Packaging
Felt surfaces and edges should be checked for contamination, loose material or damage that could enter the lamination stack.
Validate with Actual Lamination
Dimensional inspection alone cannot demonstrate complete process compatibility. Production-card testing remains the most useful final validation.
OEM & Custom Wool Silicone Press Pads
Custom Length & Width
Pads can be cut according to the lamination plate or cassette dimensions supplied by the buyer.
Custom Thickness
Standard 3mm, 5mm, 8mm and 10mm options are currently listed, while other thicknesses can be reviewed according to project requirements.
Custom Density
The existing Wallis page states that density can be customized. If density or hardness is process-critical, define the required measurable parameter in the purchase specification.
Custom Shape & Machine Cut-Outs
Rectangular pads and custom-cut shapes can be reviewed for machines requiring specific corners, holes or clearance areas.
Card Lamination Production & Export Support
Wallis supplies card-material products and card-production consumables for international card manufacturers. Buyers can combine technical drawings, existing pad samples and production parameters when requesting replacement or customized wool-silicone press pads.
Customer Feedback
For B2B orders, performance feedback is most useful when it includes the card material, laminator model, pad thickness, press temperature, pressure and number of completed cycles. These details help separate product performance from differences in processing conditions.
Packaging for Wool Silicone Press Pads
Wool silicone pads should be protected against moisture, contamination, folding, edge damage and excessive compression during storage and international transportation.
Keep Pads Flat
Large pads should be packed flat where practical to reduce deformation before installation.
Moisture Protection
Appropriate wrapping can help keep the wool-felt component dry during storage and international transport.
Protect Silicone Contact Surfaces
Keep dust, sharp objects and abrasive materials away from the silicone surface to reduce the risk of defects during later lamination use.
FAQ About Wool Silicone Press Pads for Card Lamination
What is a wool silicone press pad?
It is a heat-resistant cushion used in hot-press plastic-card lamination. The current Wallis product combines silicone with a wool felt base to provide thermal resistance and mechanical cushioning.
What materials make up the Wallis pad?
The current Wallis specification describes heat-resistant silicone combined with a wool felt base. Exact layer orientation and material composition are not published on the current page.
What temperatures can the wool silicone pad handle?
The current product table states suitability for typical PVC, PETG and PC card lamination temperatures up to approximately 180°C. Confirm actual continuous and peak operating conditions before ordering.
Are 3mm, 5mm, 8mm and 10mm pads available?
Yes. These four thicknesses are currently listed, and custom thickness can also be discussed.
Which thickness should I choose?
Selection depends on the laminator, plate clearance, existing approved pad, card stack, hardness, temperature and pressure. A thicker pad is not automatically better.
Can pad dimensions be customized?
Yes. Wallis supports customized length, width and shapes according to lamination-plate requirements.
Can the density be customized?
The existing page states that density can be customized. Buyers should specify a measurable target when density or hardness is process-critical.
What is the Shore hardness?
A specific Shore A hardness is not published for the current Wallis wool-silicone pad. Request the appropriate value for the selected construction if hardness is required in your technical specification.
Is this pad suitable for PVC cards?
Yes. PVC card lamination is one of the primary applications listed by Wallis.
Can it be used for PETG cards?
Yes. PETG is also included in the current application range. Validate the pad with the actual PETG lamination recipe.
Can it be used for PC cards?
PC card lamination is listed as an application, but actual process temperature must remain compatible with the pad's technical limits.
Is it suitable for RFID and smart cards?
It can be evaluated for RFID and smart-card lamination where cushioning is required to accommodate small local thickness variations in the card structure.
Can it be used for overlay-film lamination?
Yes. Overlay-film lamination is explicitly included in the current Wallis application information.
What is the difference between wool-silicone and pure silicone pads?
Wool-silicone pads include a felt cushioning component, while silicone-only pads do not use the wool-felt structure described on this page. Their pressure compensation, heat-transfer behavior and maintenance requirements can therefore differ.
What is the difference from a silicone-fiberglass cushion?
Silicone-fiberglass pads use fiberglass reinforcement, while this product uses wool felt as its cushioning component. The two constructions should be evaluated separately for thickness, hardness, thermal response and compression.
How many lamination cycles will the pad last?
The current Wallis page does not publish a guaranteed cycle count. Service life depends on temperature, pressure, cycle time, pad thickness, maintenance and storage.
How do I know when the pad should be replaced?
Replace or evaluate the pad when it shows excessive permanent compression, hardened or damaged silicone, contaminated felt, loose fibers, edge damage or declining lamination consistency.
How should the wool silicone pad be stored?
Keep it clean, dry and flat, away from sharp objects, contamination, uncontrolled humidity and excessive heat when it is not being used.
What is the MOQ?
The current page describes flexible ordering for small and bulk quantities but does not publish one fixed MOQ. Confirm the current MOQ according to size, thickness and customized requirements.
What information is required for a quotation?
Provide laminator model, plate dimensions, pad thickness, required quantity, card material, hot-press temperature, pressure, dwell time, existing pad specification, custom holes or shapes and delivery destination.
Can I send an existing pad for matching?
Where practical, an existing approved pad sample or detailed drawing can help Wallis evaluate dimensions, thickness and construction for a replacement product.
Request Wool Silicone Press Pad Samples & Factory Pricing
Looking for a reliable wool silicone press pad manufacturer for card lamination? Send Wallis your laminator model, pad dimensions, thickness, operating temperature, card material and quantity for technical review, sample testing and B2B factory pricing.