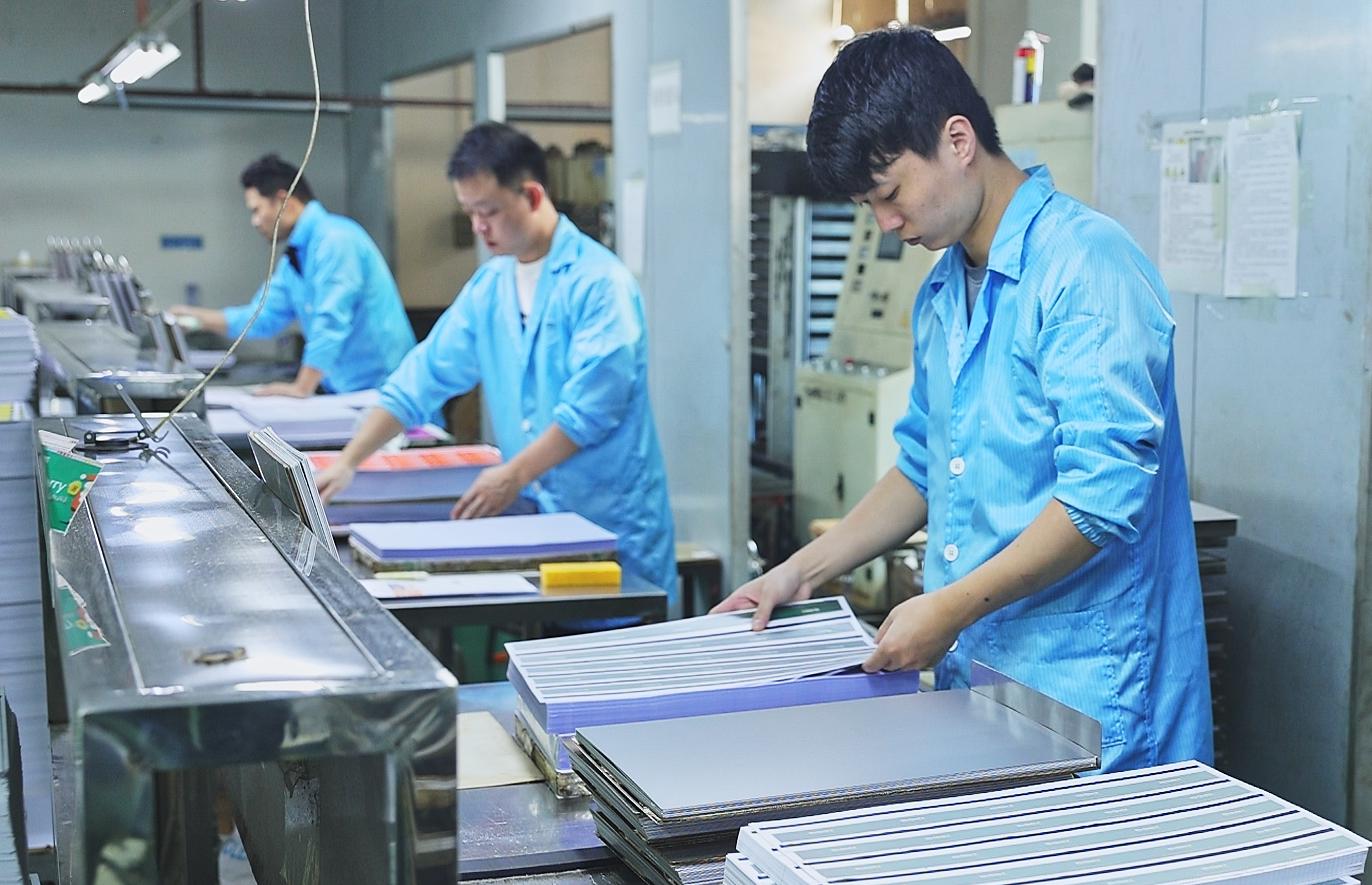
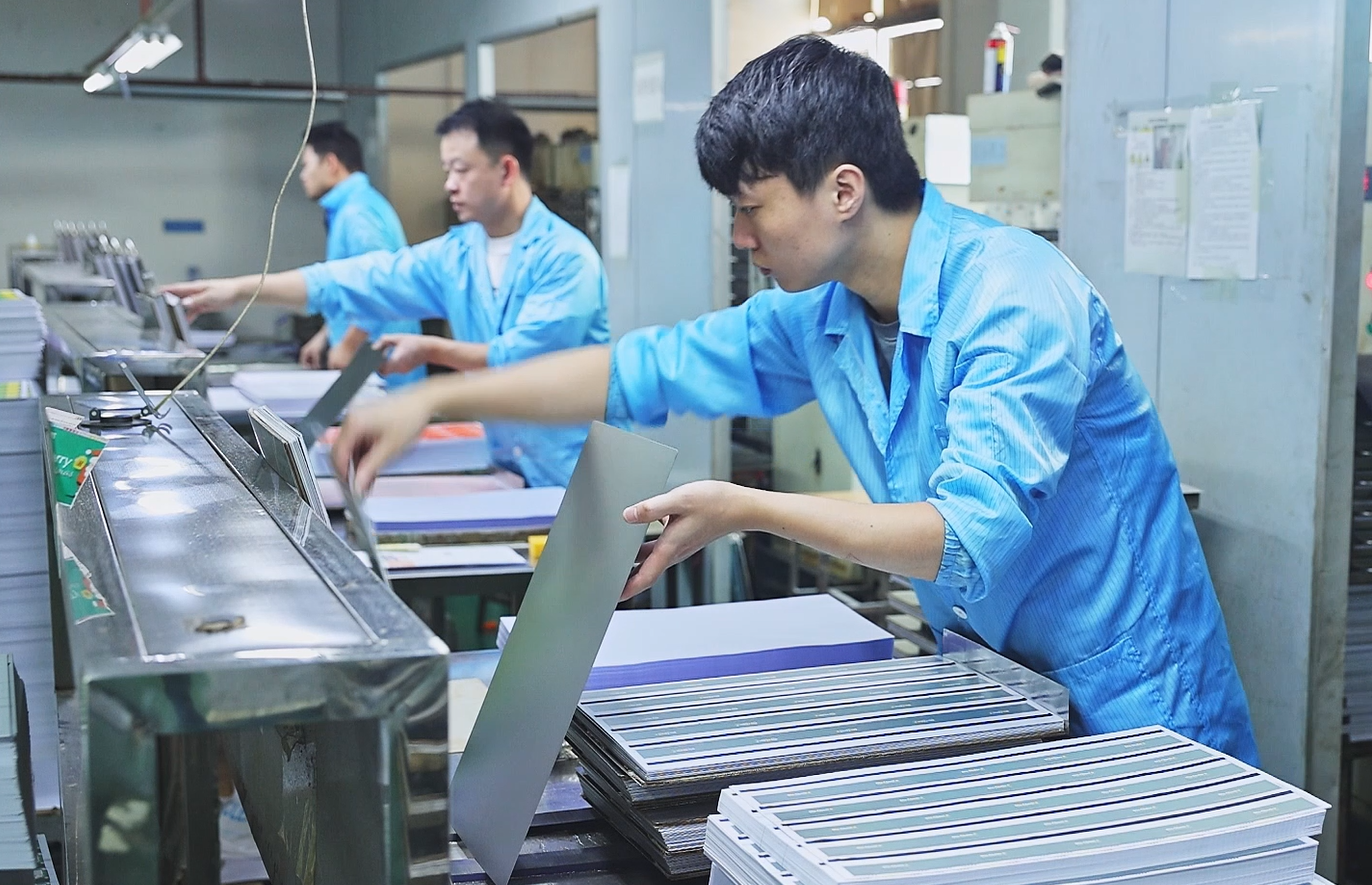
Card Lamination Cushion Pad for Consistent Plastic Card Pressing
Wallis card lamination cushion pads are reusable press consumables used in industrial plastic card laminators to help compensate for minor thickness variation and distribute pressure more evenly across the lamination cassette. Available silicone, fiberglass-reinforced and related constructions can be customized for PVC, PETG, PC, RFID inlay, ID card and smart card production.
For B2B card manufacturers, pad selection should be based on the laminator, steel plate dimensions, card material, stack construction, temperature curve, pressure, cycle time and required surface finish. A suitable press pad can support repeatable bonding and flatness, but it does not replace correct ink drying, moisture control, plate maintenance or an approved lamination recipe.
Card Lamination Cushion Technical Specifications
The following values reflect the current product-page reference range. Final material construction, continuous working temperature, hardness, dimensional tolerance and service conditions should be confirmed in the quotation, technical data sheet and approved sample.
| Parameter | Reference Specification / B2B Confirmation |
| Product | Card lamination cushion pad / card press pad |
| Reference Construction | Heat-resistant silicone with fiberglass reinforcement; other cushion constructions subject to project review |
| Reference Thickness | 1.5–3.5mm; select according to cassette gap, pressure compensation and heat-transfer target |
| Reference Working Temperature | 120–180°C for the current product range; confirm continuous and peak temperature for the selected grade |
| Surface | Smooth or matte; confirm which side faces the plate and whether release treatment is required |
| Color | White, grey or project-specific option |
| Hardness / Cushioning | Customized; specify Shore hardness or an approved compression-recovery reference where applicable |
| Size | A4, A3, press-plate size or custom cutting based on customer drawing |
| Applications | PVC, PETG, PC, ABS, RFID inlay, contactless, ID, membership and other laminated card structures |
| Reusability | Reusable under approved conditions; replacement interval depends on heat, pressure, contamination, storage and cycle count |
| Order Requirement | MOQ, packing and lead time depend on dimensions, construction and customization |
What Is a Card Lamination Cushion Pad?
A card lamination cushion pad is a heat-resistant, compressible layer installed in the lamination cassette or press stack according to the machine design. It normally works together with heating platens, polished or matte steel plates, release layers and the card-sheet booklet. Its role is to accommodate small variations in the stack and help transmit pressure and heat more consistently.
The exact installation position must follow the laminator and cassette instructions. A press pad is generally positioned outside the card booklet and steel finishing plates rather than used as an unverified direct-contact surface on printed overlays.
Pressure Equalization Across the Cassette
A controlled cushioning layer can compensate for minor plate, stack and sheet variations. This helps reduce local high-pressure and low-pressure zones that may contribute to uneven bonding, edge defects or plate marks.
Thermal Response and Cycle Time
Pad thickness and construction affect how quickly heat reaches the card stack and how the stack cools. A thinner or more conductive construction may support shorter cycles, while a thicker, softer construction may provide more compensation. The correct balance must be established through press trials rather than thickness alone.
A Process Aid, Not a Standalone Defect Cure
A cushion pad cannot by itself guarantee bubble-free or warp-free cards. Moisture, solvent retention, ink film thickness, overlay chemistry, trapped air, platen parallelism, heating uniformity, pressure, cooling and release timing must also be controlled.
![Card lamination cushion pad position and pressure distribution reference]()
How to Select the Right Lamination Press Pad
| Pad Category | Typical Selection Logic | Points to Confirm |
| Silicone + Fiberglass Pad | General card lamination where stable cushioning, clean handling and reusable performance are required | Thickness, hardness, temperature, surface tack, fiberglass exposure and compression recovery |
| Wool / Felt + Silicone Pad | Processes needing a softer buffer or different thermal behavior | Moisture control, lint generation, surface orientation, thickness loss and cleaning method |
| Thin Fast-Cycle Pad | Short press cycles where rapid heat transfer is more important than high compensation | Cassette flatness, platen uniformity, card-stack variation and peak pressure |
| High-Temperature Multilayer Pad | Higher-temperature or demanding repeated cycles when a specified construction is approved | Continuous versus peak rating, outer-layer integrity, contamination control and release behavior |
Match the Laminator and Plate Dimensions
Provide the heating plate or cassette dimensions, usable press area, positioning holes, corner radius and required clearance. Oversized pads may wrinkle or interfere with loading, while undersized pads can create pressure discontinuities near the edges.
Choose Thickness and Hardness Together
Thickness describes the physical build, while hardness and compression behavior determine how the pad responds under load. A thicker pad is not automatically better. Excess compression can alter heat transfer, stack height and final card thickness, while an overly hard pad may provide insufficient compensation.
Confirm Temperature, Pressure and Cycle Profile
Specify preheat, hot-press, cooling and release conditions, including temperature, pressure, dwell time and cycles per shift. Continuous service temperature should be distinguished from a short peak-temperature rating.
Control Surface Cleanliness and Release
Low surface contamination is essential because dust, silicone residue, damaged fibers or embedded particles can transfer defects into plates or card sheets. Confirm cleaning agents and whether the selected pad needs a dedicated orientation or release surface.
![Card lamination cushion pad material construction and production benefits]()
Silicone-Fiberglass vs Wool-Silicone Lamination Cushions
| Selection Factor | Silicone-Fiberglass Construction | Wool / Felt-Silicone Construction |
| General Character | Reinforced elastomeric pad with controlled surface and dimensional support | Softer textile-based buffer combined with heat-resistant elastomer |
| Pressure Compensation | Depends on silicone formulation, layer count, hardness and thickness | May provide a softer response; confirm permanent compression after repeated cycles |
| Heat Transfer | Can be selected for balanced or faster thermal response | May insulate more depending on felt density and thickness |
| Cleanliness | Inspect for exposed reinforcement, surface damage and silicone transfer | Inspect for lint, absorbed moisture and surface contamination |
| Best Practice | Run the same approved card stack on both candidate pads and compare heating time, flatness, bonding, plate marks and cycle stability |
Production Benefits and Practical Limits
More Uniform Pressure Distribution
A correctly selected pad can help the press apply force more uniformly across the usable sheet area, supporting more consistent layer bonding and thickness.
Protection for Lamination Plates and Card Stacks
The compliant layer can reduce hard point contact and help protect polished steel plates from localized loading. This is particularly relevant for RFID prelam sheets with chips, modules or local thickness variation, although plate hardness and stack design remain important.
Repeatable Results Across Production Cycles
Controlled pad condition helps make the lamination recipe more repeatable. Cycle records should include pad identification, first-use date, cycle count, orientation and inspection status.
No Absolute Bubble-Free Guarantee
Bubbles and watermarks can also result from moisture, incomplete ink curing, volatile release, incorrect heating rate, insufficient venting or premature cooling release. Troubleshooting must assess the full process.
Recommended Lamination Cassette Setup and Validation
The stack arrangement varies by press and card structure. Use the machine manual and an approved process sheet. The following workflow is a B2B validation framework, not a universal stack recipe.
| Step | Validation Action | Record |
| 1. Measure | Check pad thickness at multiple points, plate flatness and cassette clearance | Thickness map and equipment ID |
| 2. Build Stack | Load pad, steel plates, release layers and card booklet in the approved orientation | Stack drawing and layer direction |
| 3. Trial Press | Use the target card material, ink, overlay, RFID inlay and production dimensions | Temperature, pressure, dwell and cooling curve |
| 4. Inspect | Check bonding, flatness, gloss/matte transfer, bubbles, watermarks, dents and edge condition | Defect map and sample photos |
| 5. Approve | Lock the pad grade and process against a Golden Sample | Approved specification and change-control record |
Applications in Plastic and Smart Card Manufacturing
PVC, PETG, ABS and PC Card Lamination
The pad can be evaluated for multilayer plastic cards using compatible core sheets and overlays. Each polymer has a different thermal window, so one pad and press recipe should not be assumed to suit every material.
RFID and Contactless Smart Card Prelam
RFID sheets may contain local thickness variation around chips, antenna joints or modules. Cushion selection should be validated together with steel-plate hardness, stack height and RF testing before and after lamination.
Bank, ID, Access and Membership Cards
For programs with strict cosmetic and dimensional requirements, define acceptance limits for flatness, thickness, peel strength, surface finish and card-body defects. Compliance with any banking or government standard depends on the complete card program, not the cushion pad alone.
Troubleshooting Card Lamination Defects
| Observed Issue | Possible Pad-Related Cause | Other Process Checks |
| Uneven Bonding / Edge Lift | Pad thickness variation, permanent set, undersized pad or incorrect hardness | Platen parallelism, pressure, overlay chemistry, edge alignment and cooling |
| Bubbles / Watermarks | Contaminated or moisture-affected pad; inappropriate thermal response | Ink drying, material moisture, trapped air, heating rate and venting |
| Warped Cards | Uneven pad compression or asymmetric pad arrangement | Material shrinkage, unbalanced layers, cooling pressure and release temperature |
| Plate Marks / Dents | Embedded debris, exposed fibers or damaged pad surface | Steel-plate damage, RFID module height and handling cleanliness |
| Slow Heat-Up | Pad too thick or too insulating for the target cycle | Heater output, thermocouple accuracy, stack mass and platen condition |
| Yield Changes Over Time | Compression set, hardening, cracks or contamination after repeated cycles | Recipe drift, raw-material batch changes and equipment calibration |
Custom Size, Thickness and OEM Supply
Wallis can review custom pad dimensions, thickness, hardness, surface, color, edge shape and packing. To avoid an unsuitable quotation, provide the actual press and process information rather than requesting a pad only by A3 or A4 size.
| RFQ Information | Details to Provide |
| Laminator | Brand, model, heating/cooling method and cassette type |
| Plate / Pad Size | Length, width, corner radius, holes, slots and edge clearance drawing |
| Card Materials | PVC, PETG, ABS, PC, RFID prelam, overlay type and total stack thickness |
| Press Recipe | Hot and cooling temperature, pressure, dwell time and cycles per shift |
| Current Pad | Material, thickness, hardness, service life, photos and current defects |
| Acceptance Target | Flatness, surface finish, peel strength, cycle time and expected replacement criteria |
| Order Details | Sample quantity, bulk quantity, packaging, labeling and destination |
Quality Control, Golden Sample and Replacement Criteria
Incoming Pad Inspection
Check dimensions, thickness at several points, surface condition, edge quality, color, orientation marking and visible reinforcement. Where specified, compare hardness or compression behavior with the approved sample.
Golden Sample Approval
Run representative card sheets using the target press recipe. Approve the pad only after comparing heating response, finished card flatness, bonding, surface transfer and defects against the project Golden Sample.
When to Replace a Reusable Cushion Pad
Replace or quarantine the pad when it develops permanent thickness loss, uneven compression, cracks, exposed fibers, hardened areas, embedded contamination, edge damage or a measurable change in lamination yield. Service life should be tracked by actual cycles and condition rather than a universal fixed number.
![Wallis customer team and exhibition support for card lamination materials]()
Why Source Card Lamination Consumables from Wallis
Wallis supplies card-production materials such as core sheets, overlays, RFID inlays, lamination steel plates and press pads. This enables B2B buyers to review the cushion pad together with the complete card stack instead of evaluating it as an isolated accessory.
For project qualification, request a pad sample, technical specification, cutting drawing and test plan. Production claims such as service life, defect reduction and cycle-time improvement should be confirmed on the customer’s machine and approved card structure.
![Customer reviews for Wallis card material and lamination cushion supply]()
Frequently Asked Questions About Card Lamination Cushion Pads
What is a card lamination cushion pad used for?
It is a reusable or semi-reusable press layer that helps distribute pressure and manage heat transfer within an industrial card lamination cassette. It works with the steel plates, release layers and card booklet according to the machine-specific stack design.
Is a lamination cushion the same as a steel lamination plate?
No. The cushion is a compliant pressure-compensation material, while the steel plate transfers the selected gloss, matte or patterned finish and provides a hard, flat surface around the card stack.
Where should the cushion pad be placed in the press stack?
Placement depends on the laminator and cassette design. Follow the machine manual and approved stack drawing. The pad is generally installed outside the card booklet and finishing plates, not used as an unverified direct-contact layer on printed card surfaces.
Can one cushion pad be used for PVC, PETG and polycarbonate cards?
A pad may be evaluated across several materials, but the press recipe and thermal response differ. Validate each PVC, PETG, ABS or PC card structure separately before production.
What thickness should I choose?
The current reference range is 1.5–3.5mm. Selection depends on cassette clearance, stack variation, pad hardness, pressure, heating speed and desired compensation. A thicker pad is not automatically better.
What working temperature can the pad withstand?
The current page reference is 120–180°C. The continuous and peak temperature rating must be confirmed for the selected construction and compared with the actual press cycle.
Can the cushion pad eliminate bubbles and watermarks?
It can help improve pressure and thermal consistency, but it cannot guarantee defect-free cards. Moisture, ink curing, trapped air, heating rate, cooling and material compatibility must also be controlled.
How long can a card lamination cushion be reused?
There is no universal cycle count. Life depends on temperature, pressure, dwell time, cleaning, storage, pad construction and contamination. Track thickness, compression condition and production yield.
How should the pad be cleaned and stored?
Use only an approved cleaning method that does not swell, dissolve or contaminate the surface. Store the pad flat, clean and dry, away from sharp objects, heat and direct sunlight. Do not fold it.
Is the pad suitable for RFID and smart card lamination?
Yes, subject to testing. RFID inlays can have local thickness variation around chips and antenna joints, so validate the pad with the actual prelam, steel plates, press recipe and RF performance.
Can Wallis cut pads to a specific laminator size?
Custom length, width, thickness, hardness, edge shape and holes can be reviewed. Provide a dimensional drawing and machine model so the usable press area and clearances can be checked.
What information is required for a quotation?
Provide the laminator model, plate size, pad drawing, card materials, total stack thickness, temperature, pressure, cycle time, current pad data, observed defects, order quantity and destination.